Target keywords: portable cleanroom cabin, modular cleanroom equipment, FFU cleanroom price
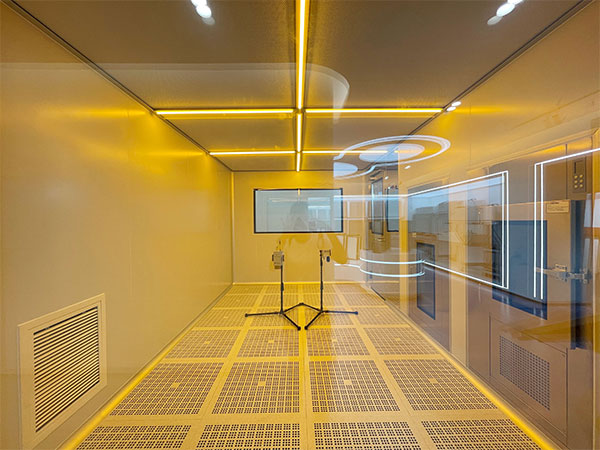
A portable cleanroom cabin beats a permanent build when the required clean zone is limited, schedules are short, processes may move, or a leased facility cannot support major construction. It can deliver ISO Class 5–8 conditions, but only after airflow, envelope, utilities, operations, and qualification are engineered as a complete system.
Air-cleanliness projects succeed when equipment performance, the surrounding facility, and daily behavior are treated as one system. For buyers searching for portable cleanroom cabin, the useful question is not only what product to buy, but what result must be maintained after installation. Particle efficiency, airflow, pressure drop, leakage, material compatibility, access, energy, testing, and operator practice all influence the outcome.
KLC International approaches portable cleanroom cabin projects by first defining the application, contaminants, operating state, available pressure, and acceptance evidence. This requirement-led method helps avoid oversizing, underperforming equipment, and documentation gaps.
Modular panels and FFUs shorten installation and limit building disruption. For procurement, this point should become a stated value or acceptance test. Recording the operating condition alongside the result also makes later troubleshooting more reliable.
Relocation value depends on reusable structure, documented disassembly, and requalification. Lifecycle planning should account for filter loading, energy, access, spares, and downtime. These factors often change the preferred option even when two products have similar initial performance.
ROI improves when a cabin avoids cleaning and conditioning unnecessary floor area. Buyers should request the test standard, operating point, tolerance, and supporting record. Without that context, apparently precise performance figures can be misleading.
The decision should be based on process risk, required performance, available space, airflow, pressure budget, operating environment, and maintenance capability. For procurement, this point should become a stated value or acceptance test. Recording the operating condition alongside the result also makes later troubleshooting more reliable.
Specifications should translate the keyword topic into measurable acceptance criteria instead of relying on a product name alone. For procurement, this point should become a stated value or acceptance test. Recording the operating condition alongside the result also makes later troubleshooting more reliable.
Installation interfaces, controls, access, cleaning, spare parts, and documentation should be resolved before purchase. The practical implication is that equipment, room airflow, and operator movement must be reviewed together. A strong component cannot compensate for bypass leakage or an uncontrolled procedure.
Start with baseline measurements, define responsibilities, and agree the test method before equipment arrives. The practical implication is that equipment, room airflow, and operator movement must be reviewed together. A strong component cannot compensate for bypass leakage or an uncontrolled procedure.
Commission the system under realistic conditions and train operators to recognize alarms, damage, and performance drift. For procurement, this point should become a stated value or acceptance test. Recording the operating condition alongside the result also makes later troubleshooting more reliable.
Trend pressure, airflow, condition, energy, and service events so replacement or optimization decisions use evidence. A site trial or representative qualification can expose interactions that drawings miss, including wake zones, moisture, dust release, door traffic, and sensor response.
|
Option or stage |
Best use |
Main advantage |
Main caution |
|
Portable cabin |
Application-specific |
Supports the target function |
Verify under real conditions |
|
Permanent room |
Application-specific |
Supports the target function |
Verify under real conditions |
|
Soft-wall booth |
Application-specific |
Supports the target function |
Verify under real conditions |
|
Clean bench |
Application-specific |
Supports the target function |
Verify under real conditions |
The table is a planning aid, not a substitute for a site-specific assessment. Ratings must be compared at the same airflow and test basis, and final performance must be verified after installation. KLC can align drawings, materials, filters, motors, controls, and documentation with the agreed operating point.
A useful request for quotation should include:
Define the contamination or process risk.
Quantify airflow, efficiency, pressure, material, and environmental limits.
Compare products using the same test basis and operating point.
Plan installation, controls, cleaning, spares, and safe maintenance.
Document acceptance tests, training, records, and change control.
Ask KLC International to identify assumptions and exclusions in the proposal. A clear quotation should distinguish factory tests from site tests, supplied components from third-party work, and nominal ratings from guaranteed values.
Inspect equipment on arrival for packaging damage, correct identification, dimensions, seals, filters, instruments, and documents. During installation, control construction dust and protect sensitive media. Commissioning should verify airflow direction and volume, differential pressure, alarms, interlocks, electrical safety, noise where relevant, and the specified cleanliness or capture performance.
After handover, use condition-based maintenance supported by scheduled inspections. Trend differential pressure and airflow, investigate abnormal changes, protect spare filters, and document replacements. Any change to media, motor speed, room layout, door operation, process equipment, or cleaning chemistry should trigger a risk review. KLC service teams can help define spares and a verification plan suited to the application.
A dependable proposal separates claims from evidence. Start by checking that drawings match the requested dimensions, airflow direction, service access, utilities, and installation interfaces. Then review performance reports for the tested model, test method, operating point, instrument status, acceptance limit, and traceable result. A corporate quality certificate may support confidence in the supplier’s processes, but it does not replace product-level data or installed-system qualification.
Also confirm how deviations and design changes will be handled. Media, adhesives, motors, sensors, frame materials, seals, and production sites can all influence performance. For critical projects, require advance change notification, serial or batch traceability, agreed inspection records, and a defined nonconformance process. Shipment protection should be part of the technical scope because crushed pleats, damaged gel, distorted frames, or moisture exposure can invalidate an otherwise compliant filter.
The commercial comparison should use total delivered value: equipment, freight, duties, installation, energy, consumables, validation, downtime, warranty response, and expected service life. This produces a more defensible decision than comparing purchase price alone and gives operations teams a realistic maintenance budget.
The most common errors are selecting by headline efficiency alone, ignoring system pressure, treating a factory certificate as proof of site performance, and leaving maintenance access until the end of design. Another mistake is assuming that more airflow or a higher filter class is always safer. Excessive airflow can create turbulence, raise energy use, and disturb processes; excessive resistance can reduce delivered flow. A balanced design is both cleaner and more reliable.
KLC International recommends documenting the design basis and acceptance criteria before ordering. That single step makes supplier comparisons fairer and gives commissioning teams a clear target.
Yes, if filter coverage, airflow, leakage, background conditions, and operations support it.
Often much faster than a permanent room, though design approval, utilities, and validation still take time.
Many systems can, but dimensions, utilities, logistics, and requalification must be planned.
Usually for limited areas and temporary needs; lifecycle cost should include moves, energy, maintenance, and validation.
Typically power and sometimes cooling, monitoring, compressed air, data, exhaust, or process services.
That depends on classification, traffic, contamination risk, and pressure strategy.
Use delivered airflow, motor efficiency, filter grade, controls, noise, testing, and lifecycle service.
Particle classification under the agreed occupancy state plus supporting integrity, airflow, and pressure tests.
Often yes if the frame, controls, electrical system, and air returns are designed for expansion.
Ignoring heat load and return-air paths can prevent the cabin from maintaining stable conditions.
Planning a project involving portable cleanroom cabin? Share the application, dimensions, airflow, target performance, operating environment, destination market, and required test documents with KLC International. The KLC team can review the specification, propose a practical configuration, and prepare a quotation that covers equipment, filters, controls, and verification needs.
Request a technical review or quotation from KLC International for Portable Cleanroom Cabin.
Technical note: Final selection and compliance should be confirmed against the current standards, regulations, process risk assessment, and site conditions applicable to the project.


 IPv6 network supported